 Bolli Automation specializes in vision dispensing machines_factory direct
Bolli focuses on Vision Fluid
BOLI, FOCUS ON VISION‑BASED FLUID DISPENSING
Search All
BOLI, FOCUS ON VISION‑BASED FLUID DISPENSING
To evaluate a vision dispensing machine, you cannot just look at how many pieces it dispenses per day. High output does not mean high efficiency—there may be a large amount ofetc. waiting, changeover, and rework。overall equipment effectiveness OEE multiplies availability, performance, and yield, it can more truly reflect the equipment contribution. This article explains how to calculate OEE, and from which directions to improve systematically.
OEE etc. equals availability times performance times yield, a multiplicative metric. any link being a short board will multiply and lower the result, so it exposes hidden losses better than single output. For managers, the value of OEE is to break ”why the expectation was not met” into three locatable blocks, rather than vaguely attributing it to ”slow equipment”. Look at OEE separately; fix the lowest block first, and improvement is targeted.
availability is the ratio after deducting failures, changeovers, material waiting, etc. downtime from planned operation time. The key to improvement isreduce unplanned machine downtime: Bolli Automation Co., Ltd. equipment stability and unlimited remote maintenance help shorten fault handling time, while a standardized changeover process can reduce changeover downtime. When counting availability, it is recommended to list changeover time as a separate item; otherwise it will be averaged into material waiting, masking the real bottleneck.
Performance is the ratio of actual cycle time to theoretical cycle time, affected byidle travel, deceleration, and small pausesaffect it。many efficiency losses come from suboptimal trajectories and frequent acceleration/deceleration; motion control optimization and dispensing order planning can significantly improve performance. Remove unnecessary pen-lifts and backtracks, and single-piece time drops. Small pauses seem only a few seconds, but accumulated over a shift they become considerable capacity loss, worth troubleshooting segment by segment with logs.
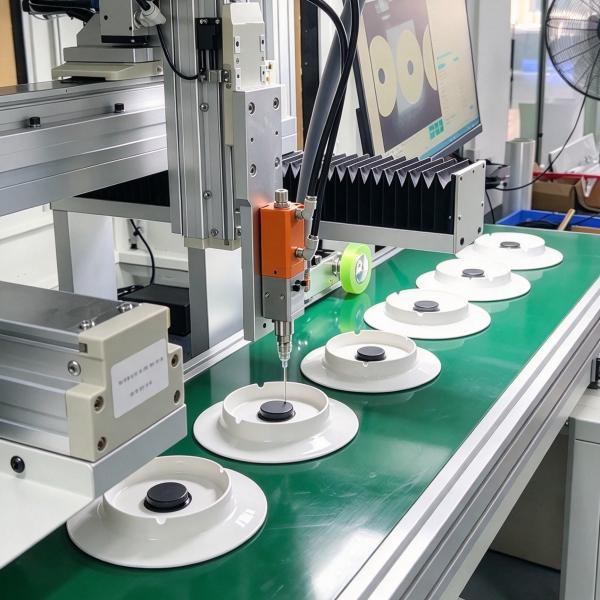
Yield is the number of first-pass good dots divided by total dots, directly related todispensing consistency and Vision positioningdirectly related. Metrological verification can promptly detect dispensing drift; changeover and program error-proofing can block wrong parameters. Doing these two things well significantly reduces rework and patch dots. Classifying defects by type can distinguish equipment problems from incoming material problems, avoiding blindly adjusting the machine and wasting time.
Shortening changeover time relies on quick clamping and program calling; reducing faults relies onpredictive maintenance and remote support ; raising yield relies onclosed-loop control plus metering calibration. the three work together, and OEE will truly rise. Bolli provides unlimited remote after-sales and training, can assist customers in building efficiency dashboards, monitoring availability, performance, and yield separately. The value of the dashboard is to make the three-line trends visible at the same time, so whoever falls behind is clear at a glance.
The vision dispensing machine's equipment utilization rate and OEE measure overall efficiency as availability × performance × yield, exposing hidden losses better than output alone. To build an efficiency dashboard, contact 13352947677 for unlimited remote after-sales and on-site sample-testing support.