 Bolli Automation specializes in vision dispensing machines_factory direct
Bolli focuses on Vision Fluid
BOLI, FOCUS ON VISION‑BASED FLUID DISPENSING
Search All
BOLI, FOCUS ON VISION‑BASED FLUID DISPENSING
Yield is not a single-point metric, butthe product of the joint effect of multiple links: incoming material, Vision, motion, dispensing, and environment. To improve yield, follow the process chain to find the shortest board, rather than just staring at the equipment's nominal precision. Whichever link is leaking, fix from that link.
common dispensing defects are: offset, broken glue, glue accumulation, stringing, bubbles, poor curing. Offset mostly belongs to Vision positioning or fixture problems; broken glue and accumulation mostly belong to dispensing valve and glue pressure; stringing mostly belongs to valve-body suck-back and temperature; bubbles belong to adhesive degassing and pipeline; poor curing belongs to adhesive ratio and temperature/humidity. Only by tracing the link from the defect can you prescribe the right remedy. It is recommended to make a defect-to-link comparison table so new employees can make initial judgments by the table, shortening troubleshooting time.
the premise of yield is "where it hits is where it counts". Through Mark point positioning, feature matching, and coordinate transformation, the vision dispensing machine compensates the actual position of the workpiece to the program coordinates. The equipment uses Hikvision industrial camera with self-developed light source; typical following positioning precision is up to millimeter level — the specific caliber varies by machine model: in-line following about ±0.5 mm, granite platform panoramic about ±0.05 mm, etc. Only with accurate positioning can we talk about yield. For multi-station or continuous production lines, it is recommended to unify the positioning reference and fixture reference to avoid cumulative errors introduced by reference switching.
within the same program, the dispensing volume of each piece must be consistent. Stable air-pressure or screw metering, constant adhesive temperature, and crisp valve-body suck-back are the three elements. For scenarios with strict gram-weight requirements, such as using Screw valve metering, regular first-piece and in-process weighing is needed to control fluctuation within the allowable bandwidth. At the same time, record the batch number and ambient temperature of each batch of adhesive to facilitate tracing the source of fluctuation.
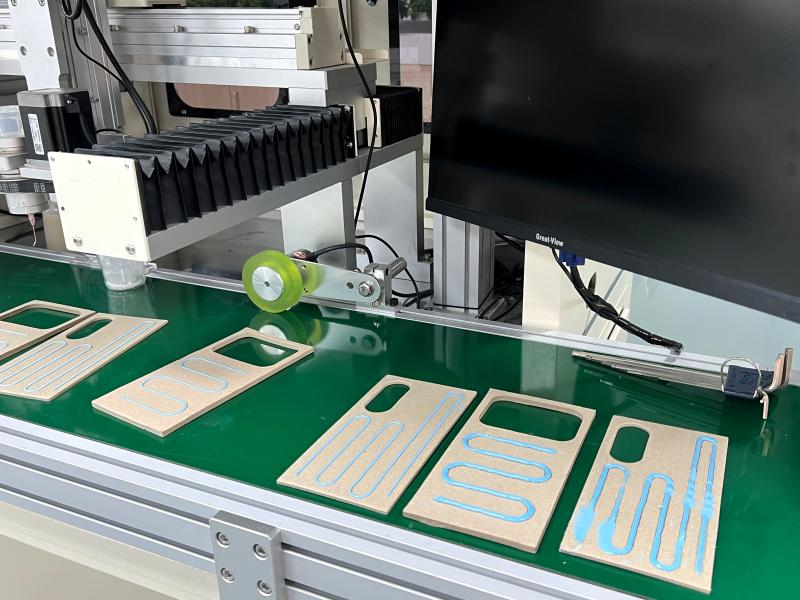
poor workpiece clamping consistency cannot be saved even by the most accurate Vision. Wear of fixture positioning surfaces and incoming material size drift will directly eat into the yield. It is recommended to regularly spot-check fixtures, do first-piece sampling inspection of incoming materials, and block upstream fluctuations outside the equipment rather than letting the equipment hard-carry. Fixture design should reserve wear compensation, and proactively replace before end of life, rather than passively fighting fires when problems occur.
temperature and humidity affect adhesive viscosity and curing; incomplete glue cleaning during changeover will cause adhesive mixing contamination. Writing temperature/humidity control, glue-cleaning process, and first-piece confirmation into standard operations is more effective than temporary fire-fighting. Bolli provides unlimited remote after-sales and training to help customers solidify the process into reproducible actions. It is recommended to establish first-piece confirmation per shift and shift-handover records, so anomalies are found at the earliest stage.
to improve dispensing yield, manage each link of the process chain as a product; locate defects to the short board and solidify standard operations. Bolli provides unlimited remote after-sales and training to assist implementation; for details, consult 13352947677.