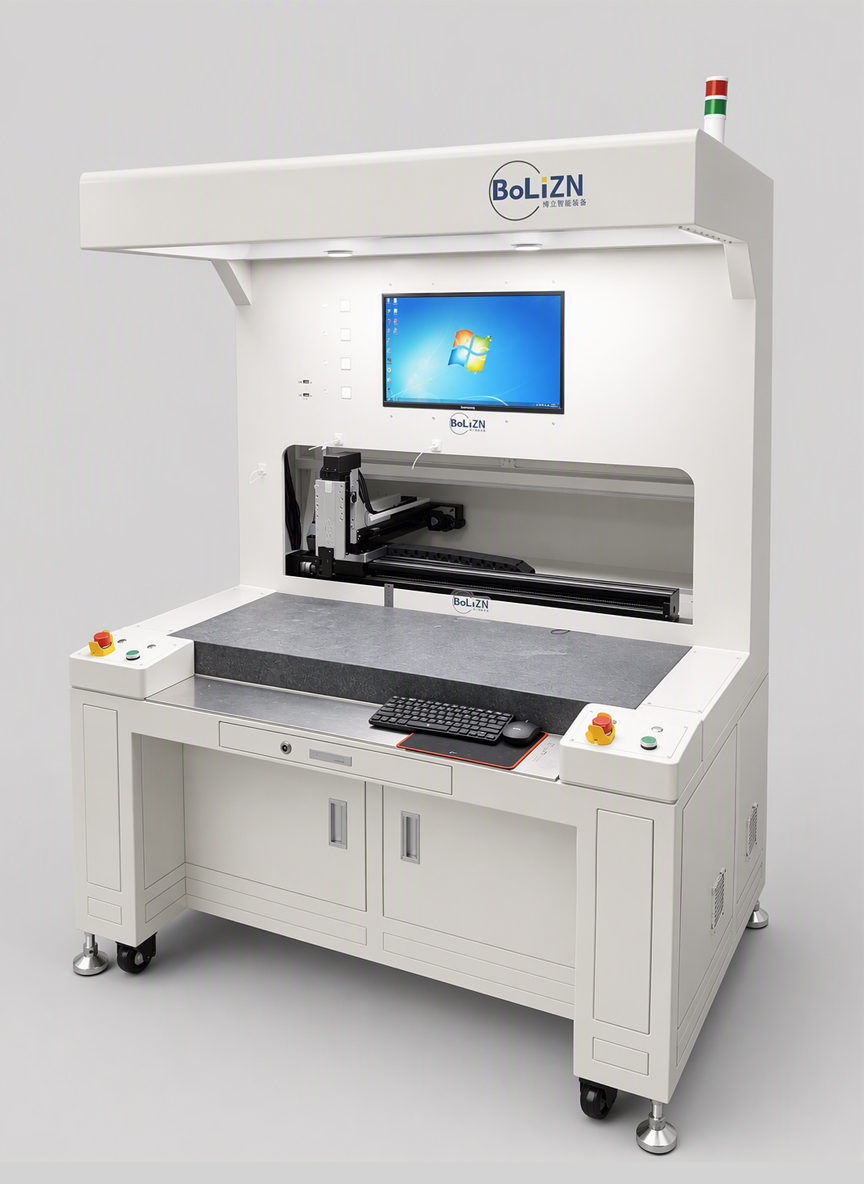
 Bolli Automation specializes in vision dispensing machines_factory direct
Bolli focuses on Vision Fluid
BOLI, FOCUS ON VISION‑BASED FLUID DISPENSING
Search All
BOLI, FOCUS ON VISION‑BASED FLUID DISPENSING
The glue shape, efficiency, and consistency of the vision dispensing machine are largely determined by process parameters. With the same equipment and adhesive, different parameters may produce vastly different glue dots. Parameters such as dispensing pressure, motion speed, temperature, and dwell time need to be set in coordination around the adhesive type and workpiece, rather than applying fixed values, let alone filling in casually by feel.
Core parameters includedispensing pressure, movement speed, adhesive temperature and ambient temperature, holding time, and needle-lift heightetc. The dispensing pressure affectsglue volume and line thickness; motion speed relates toCycle, and also affectsstringing; temperature changesglue flowability; dwell time determineswhether the glue dot is fully formed; needle-lift height relates towhether the needle release is clean. These parameters constrain each other; adjusting one often requires re-examining the others and they cannot be viewed in isolation.
Too low pressure causes broken glue and insufficient volume; too high causes overflow, thicker lines, or even splashing. To determine pressure, first refer tothe glue viscosity and needle inner diameter, then start from small samples and gradually increase pressure, observing whether the glue dots are continuous, full, and not over the boundary. Bolli's vision dispensing machine can use sample testing in trial production to confirm the pressure window item by item, record the usable range as the baseline for subsequent mass production, avoiding starting from scratch each time.
excessively fast movement speed easily causes stringing and elongates the glue shape; too slow reduces the takt and even causes local accumulation. Speed should match the dispensing volume: when the volume is large, appropriately increase speed; for micro dispensing, slow down to ensure precision. The path's rounded corners, turns and start/end positions also affect glue-shape continuity; they should be considered together when editing dispensing motions, not just looking at single-point parameters, otherwise continuity is affected.
for hot-melt adhesive etc. systems that require heating, the adhesive temperature directly affectsflowability and bonding; ambient temperature relates toglue viscosity stability and equipment baseline. Dwell time is key to glue-dot forming; too short and the adhesive does not spread fully, too long and it slows the cycle. Bolli's vision dispensing machine relies on Leadshine servo and Xinsheng lead screws to ensure motion stability, so the effects of temperature and dwell can be reflected on a consistent platform, reducing fluctuation from external disturbances.
there is no universal fixed value for parameter settings; the correct approach is to first determine the baseline with small samples, then gradually scale up to mass production, and record the glue-shape result of each parameter set during the process. When defects occur, first locate which categoryparameter deviation, then maketargeted fine-tuning, rather than starting over. Bolli provides unlimited remote after-sales and sample-testing support, and can assist enterprises in establishing a standard process for parameter debugging and review, depositing experience; you can contact Bolli Automation at 13352947677 for sample-testing and debugging advice.
when enterprises introduce a new adhesive or new workpiece, it is recommended to first do a small-batch sample test, toverify the combination of dispensing pressure, speed, temperature, holding time etc. parameters clearly, then move into mass production. Bolli's vision dispensing machine can combine sample testing to confirm the parameter window, and provide executable setting suggestions based on actual capacity, so the process falls into the stable range from the start, reducing later repeated adjustments, and facilitating the provision of complete parameter records during customer audits.